Load & assemble
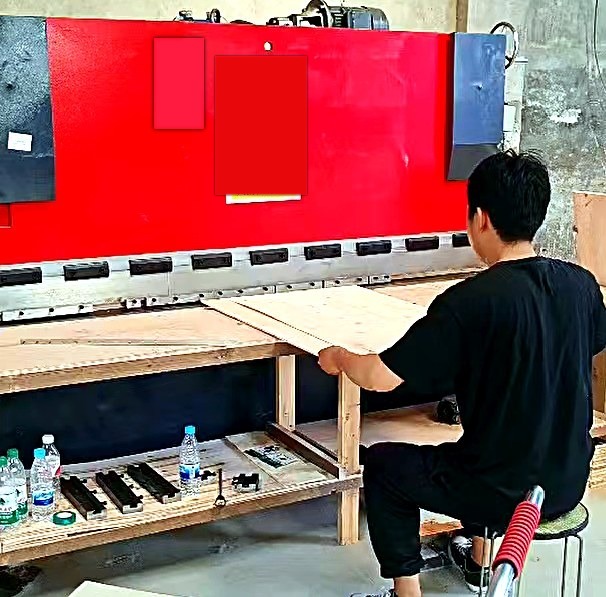
Lay the steel edge and prepared plywood on the worktable.
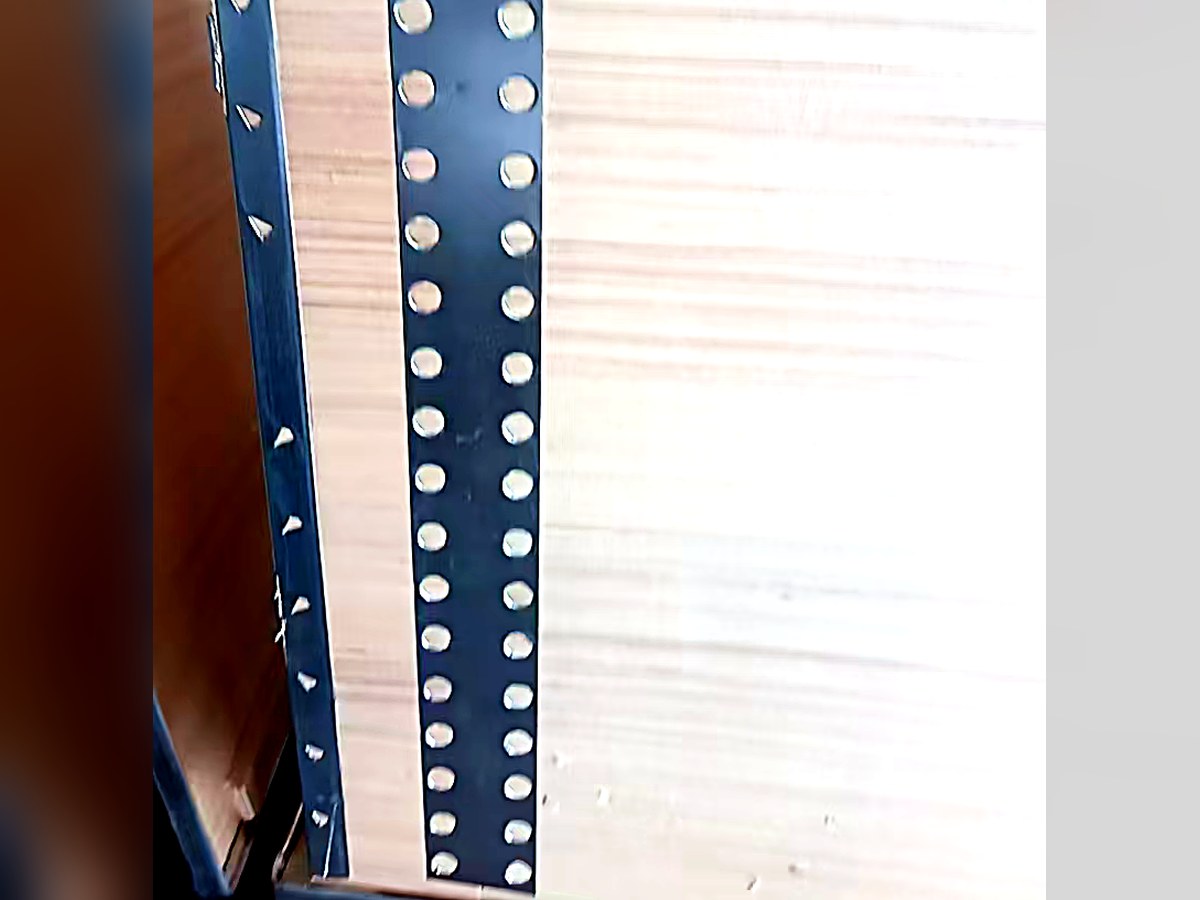
Steady hydraulic force joins preformed steel edges to plywood, giving flat, rigid panels that hold their dimensions.
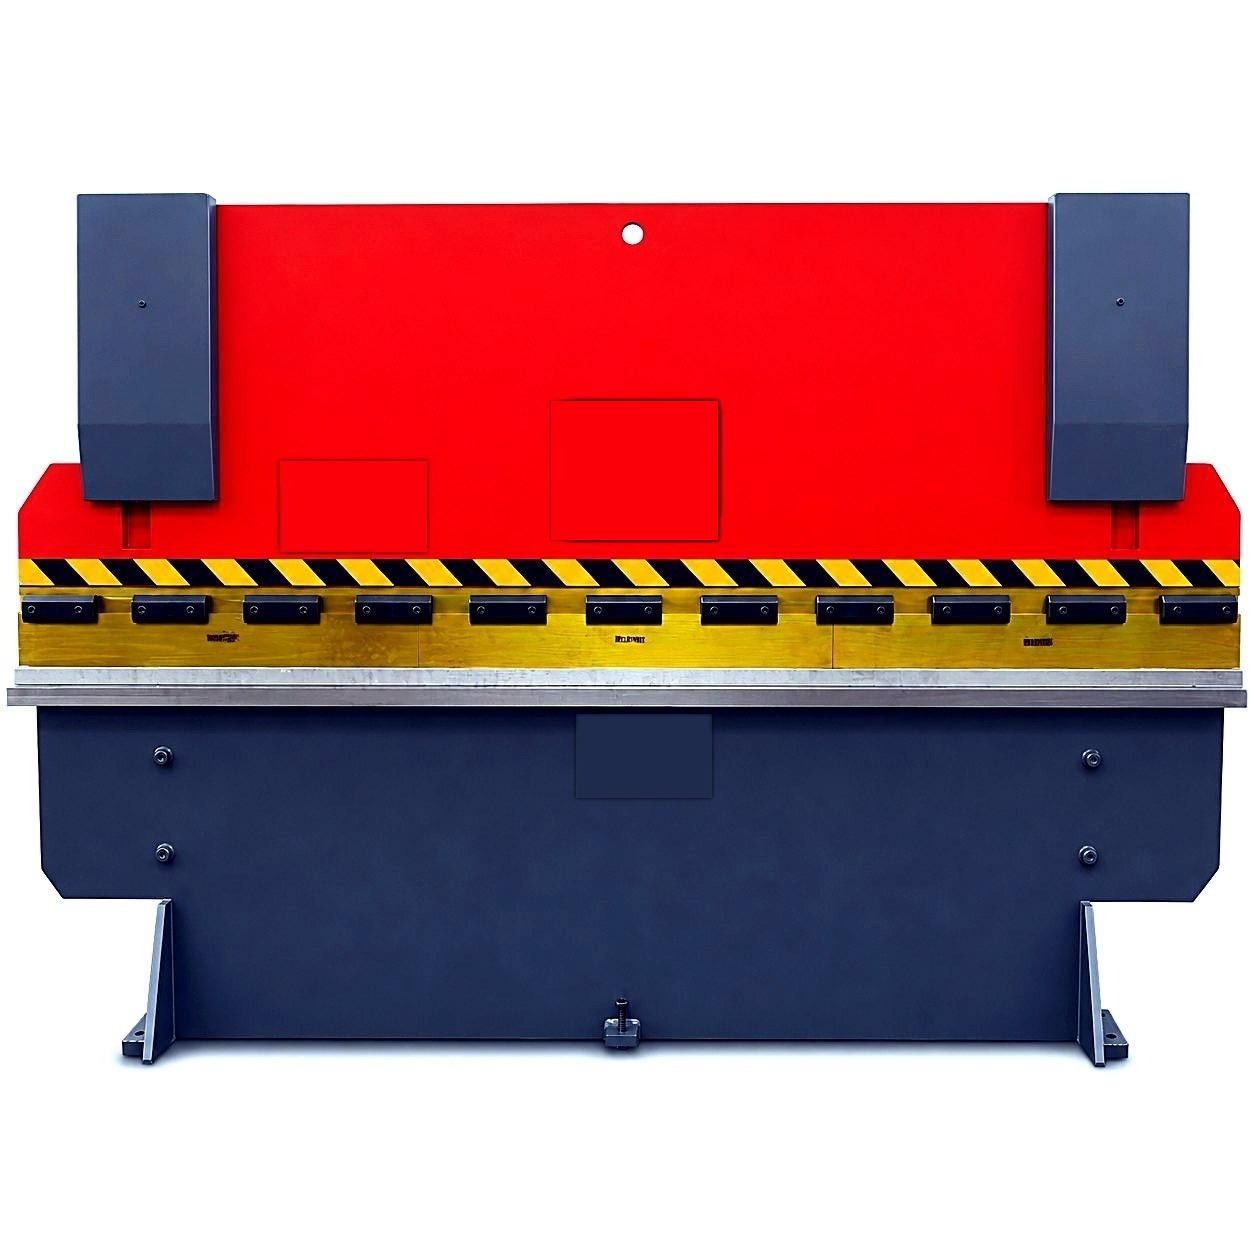
The YA2500 hydraulic press finishes the steel-edged panel: it applies steady, even force to join preformed steel edges with prepared plywood, turning out flat, rigid panels with consistent dimensions. Magnetic dies slide out for fast removal and changeover. The YA series covers three working widths — YA1600 (1.6 m, 30 tons), YA2500 (2.5 m, 30 tons) and YA3200 (3.2 m, 60 tons) — so the press fits the box size instead of one frame having to do everything.
Even pressure gives tight, repeatable assembly
Magnetic quick-change dies slide out for fast changeovers
Light curtains, emergency stops and overload protection
Three working widths (1.6 / 2.5 / 3.2 m) fit the press to the box size
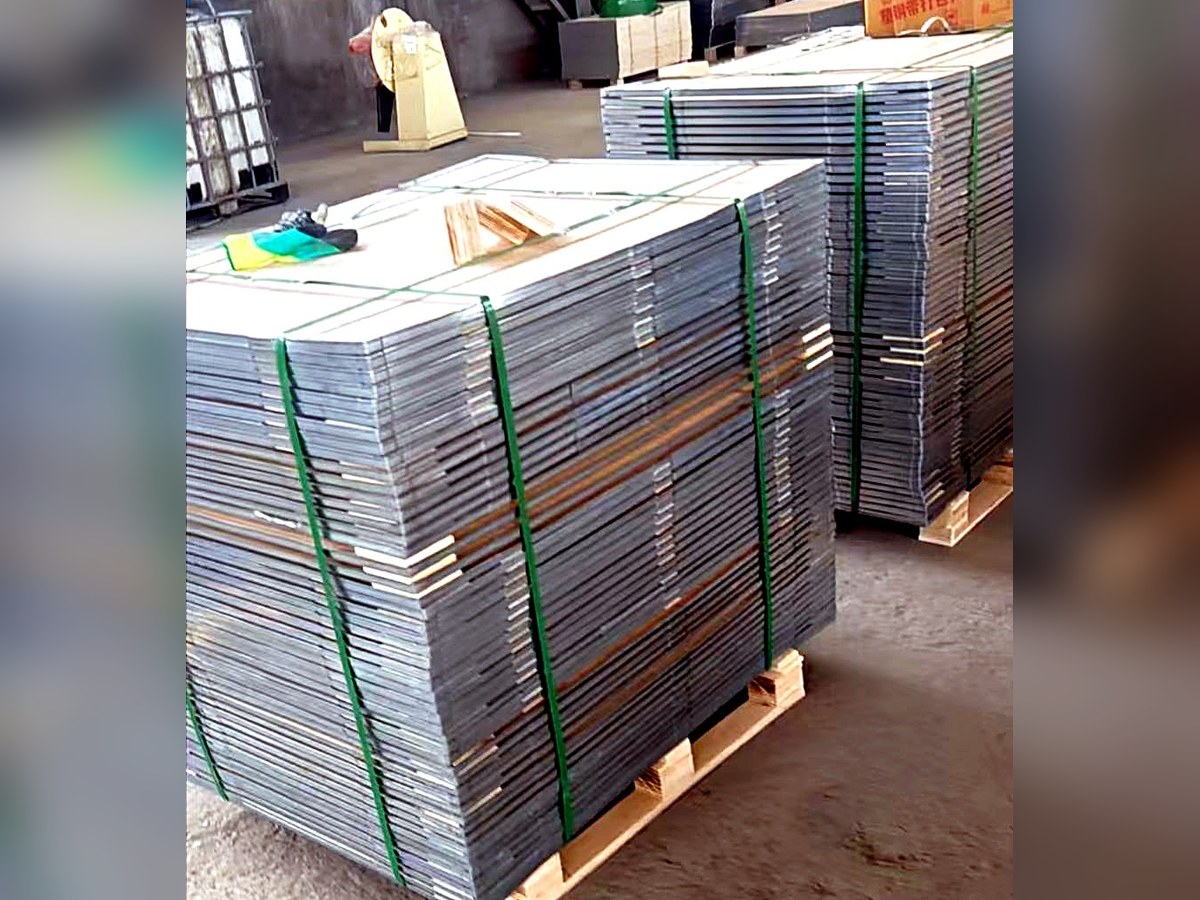
Steel-edged plywood box panels
Large export packaging cases
Heavy-duty machinery crates
Custom oversized box production
Standard configuration data. Machines are configured to order — contact us for values matched to your product.
| Model | YA2500 |
|---|---|
| Working width | 2.5 m |
| Nominal pressure | 30 tons |
| Motor power | 3 kW |
| Machine weight | 1.5 tons |
| Machine size (L×W×H) | 2,500 × 950 × 1,900 mm |
| Die system | Magnetic dies, sliding quick-change |
| Recommended working area | 3 × 3 m |
Available variants: YA1600 — 1.6 m working width, 30 tons nominal pressure; YA3200 — 3.2 m working width, 60 tons nominal pressure.
Lay the steel edge and prepared plywood on the worktable.
Mechanical stops line the components up and set the assembly gaps.
The platen comes down evenly and applies the set pressure.
After a short hold, the platen returns on its own, ready for the next panel.
Check the hydraulic oil level, lines and joints for leaks, dies and press plates for cracks, and the e-stop and wiring. Jog the cylinder up and down empty to check smooth travel.
Set the pressure valve to the value for the strip and panel thickness, and set the travel limit so the ram cannot over-press the strip or panel.
Lay the steel edge or panel to be pressed flat and centered on the die, lined up and stable.
Step on the foot switch (or press both start buttons): the ram comes down slowly and presses the strip into shape. Hold pressure 1–3 seconds, then release — the ram returns on its own.
Take the finished piece off, place the next workpiece, and repeat. Never overload the press or go past the rated stroke.
Return the ram to its top position, switch off the motor and main power. Clear iron filings and oil from the table and wipe the machine down.
Safety: keep hands, arms and head out of the ram zone during pressing. Stop immediately on oil leaks, unusual noise, low pressure or electrical faults — never run a faulty machine.