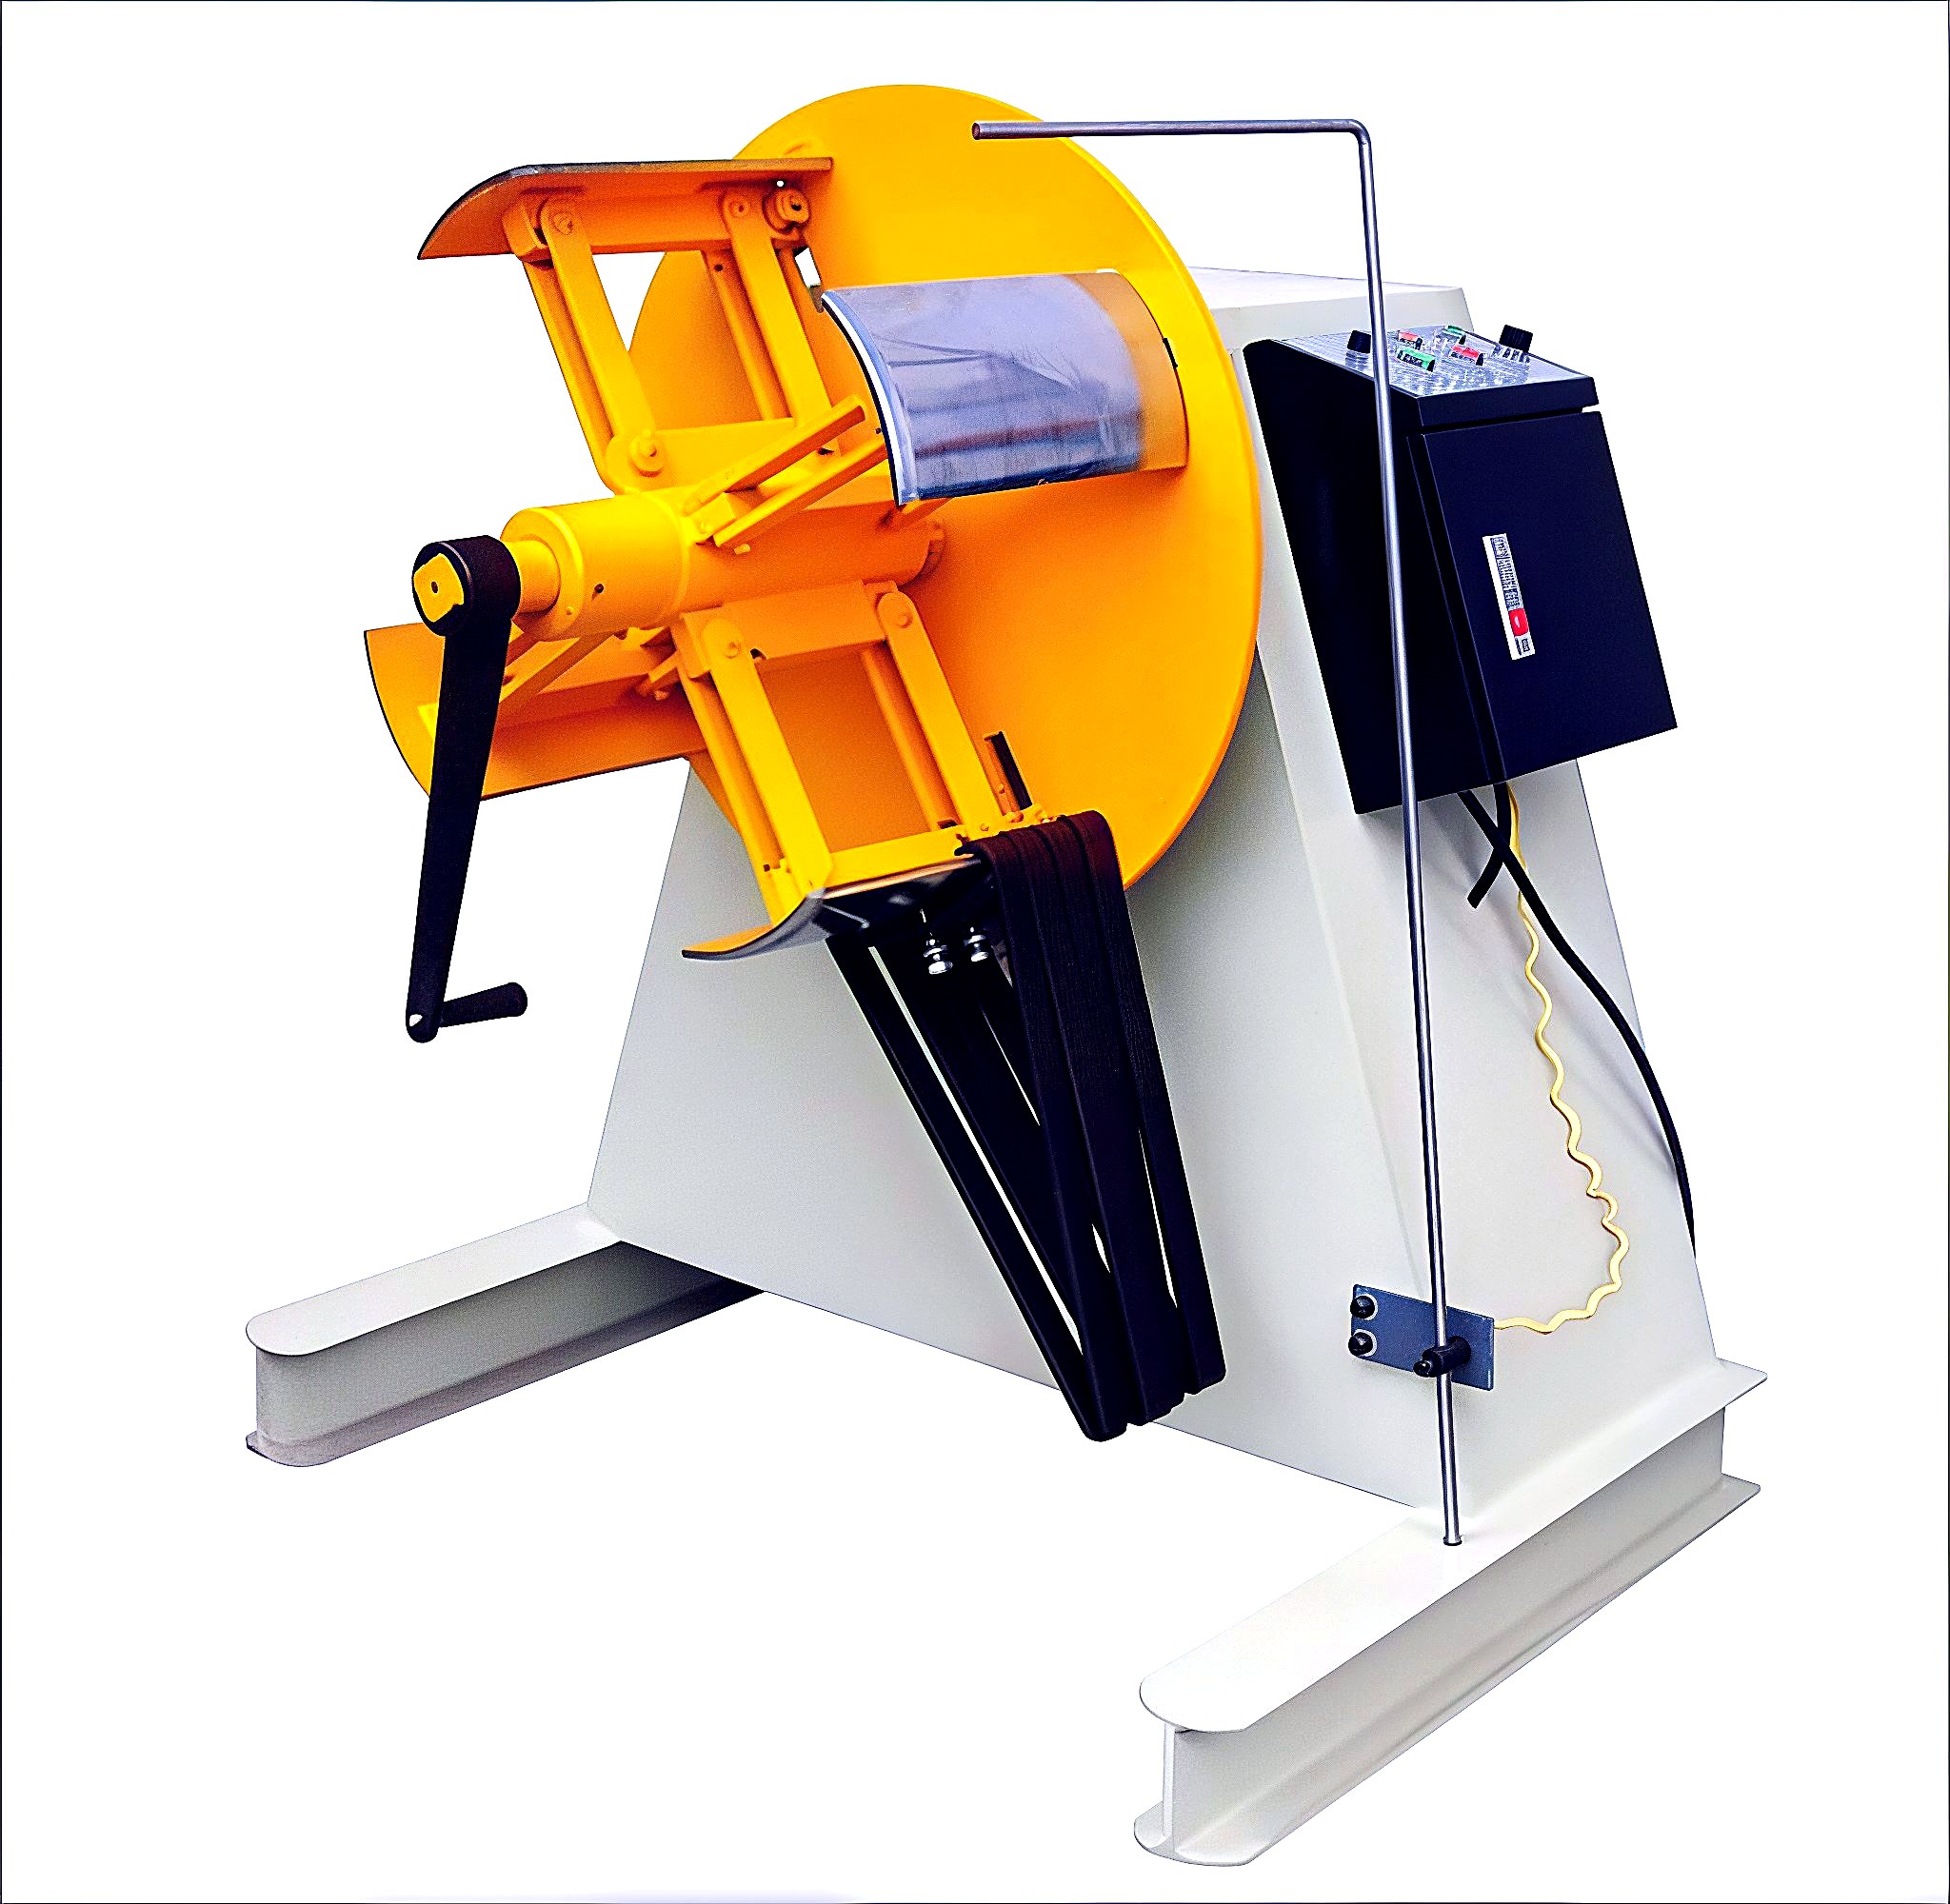
Automatic feeding
The feeder delivers galvanized steel strip to the set position.
Based on the DA-8000 buckle machine platform, with a female-buckle die and hydraulic cylinder added, so one machine turns out matched male and female buckles for nailless plywood boxes.
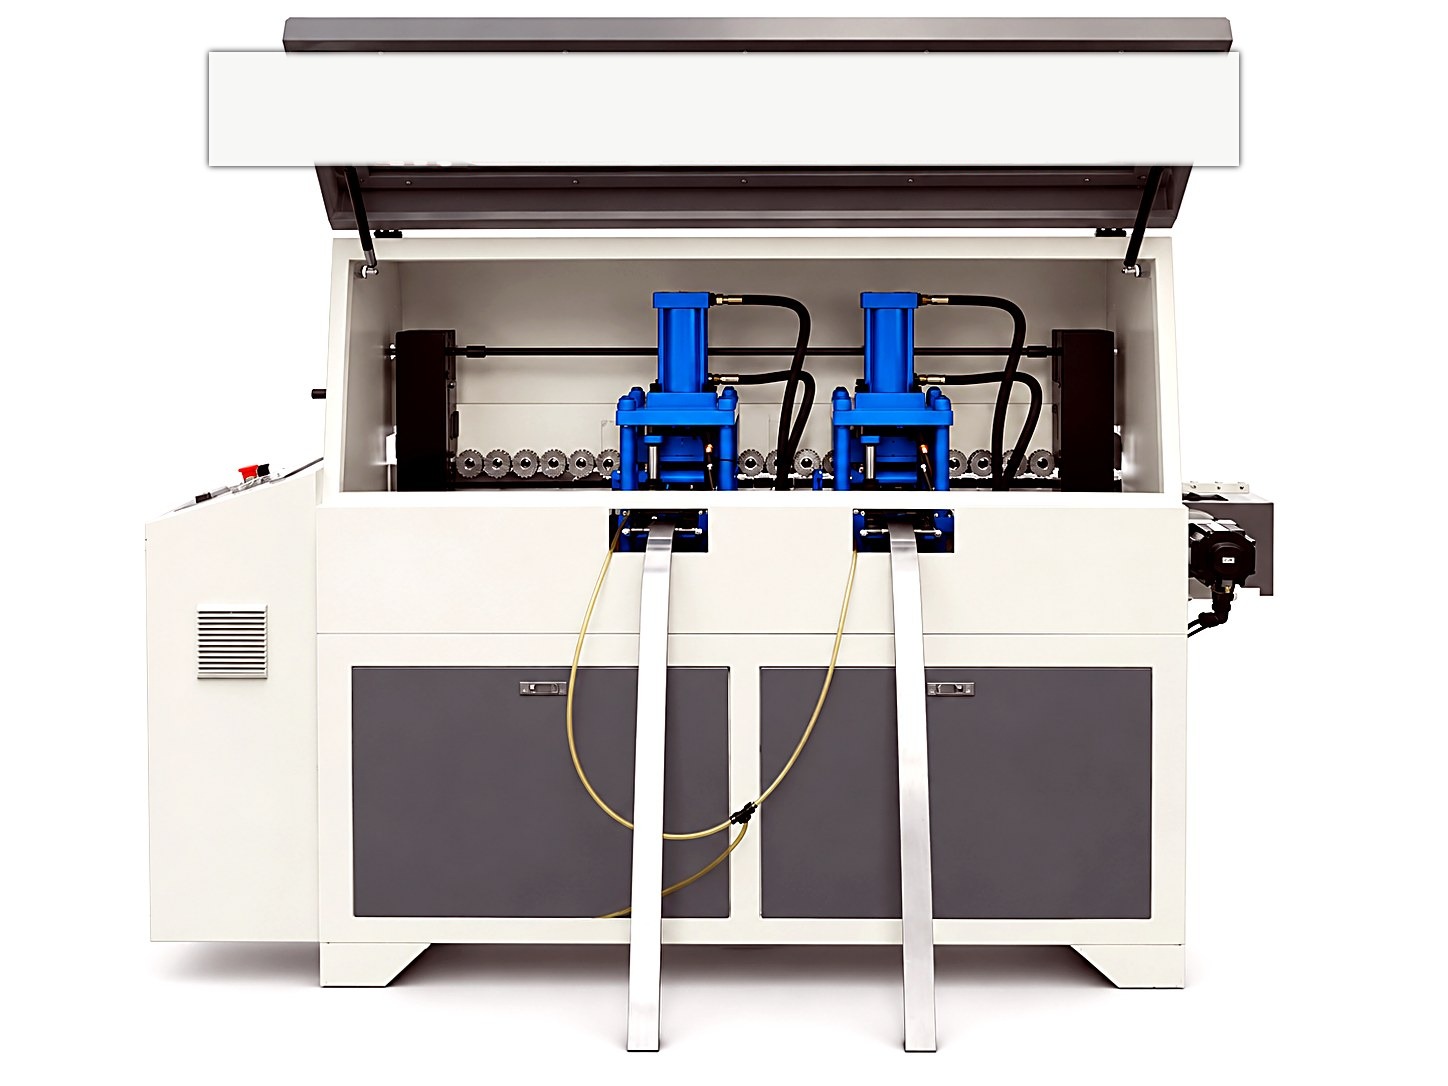
This variant keeps the DA-8000 platform — Siemens PLC control, Inovance servo drive, 6 kW drive and 30–60 fastenings per minute — and adds a female-buckle die plus an extra hydraulic cylinder. One machine therefore turns out both halves of the clasp set: male buckles and female buckles, in the same 50 mm strip and 5–12 mm panel range. The standard DA-8000 makes male buckles only; pick this variant when the box design calls for the full male–female fastening set from a single machine. Two automatic steel strip decoilers come as standard — one for each die station.
One machine turns out both male and female buckles
Same DA-8000 platform: Siemens PLC + servo positioning, 30–60 fastenings per minute
Female-buckle die and hydraulic cylinder included
Matched clasp sets improve box assembly fit and reuse life
Suits different panel thicknesses (5–12 mm) and fastener specifications
Nailless plywood boxes
Collapsible wooden boxes
Steel-edged export cases
Reusable industrial transport boxes
Buckle boxes with male–female clasps
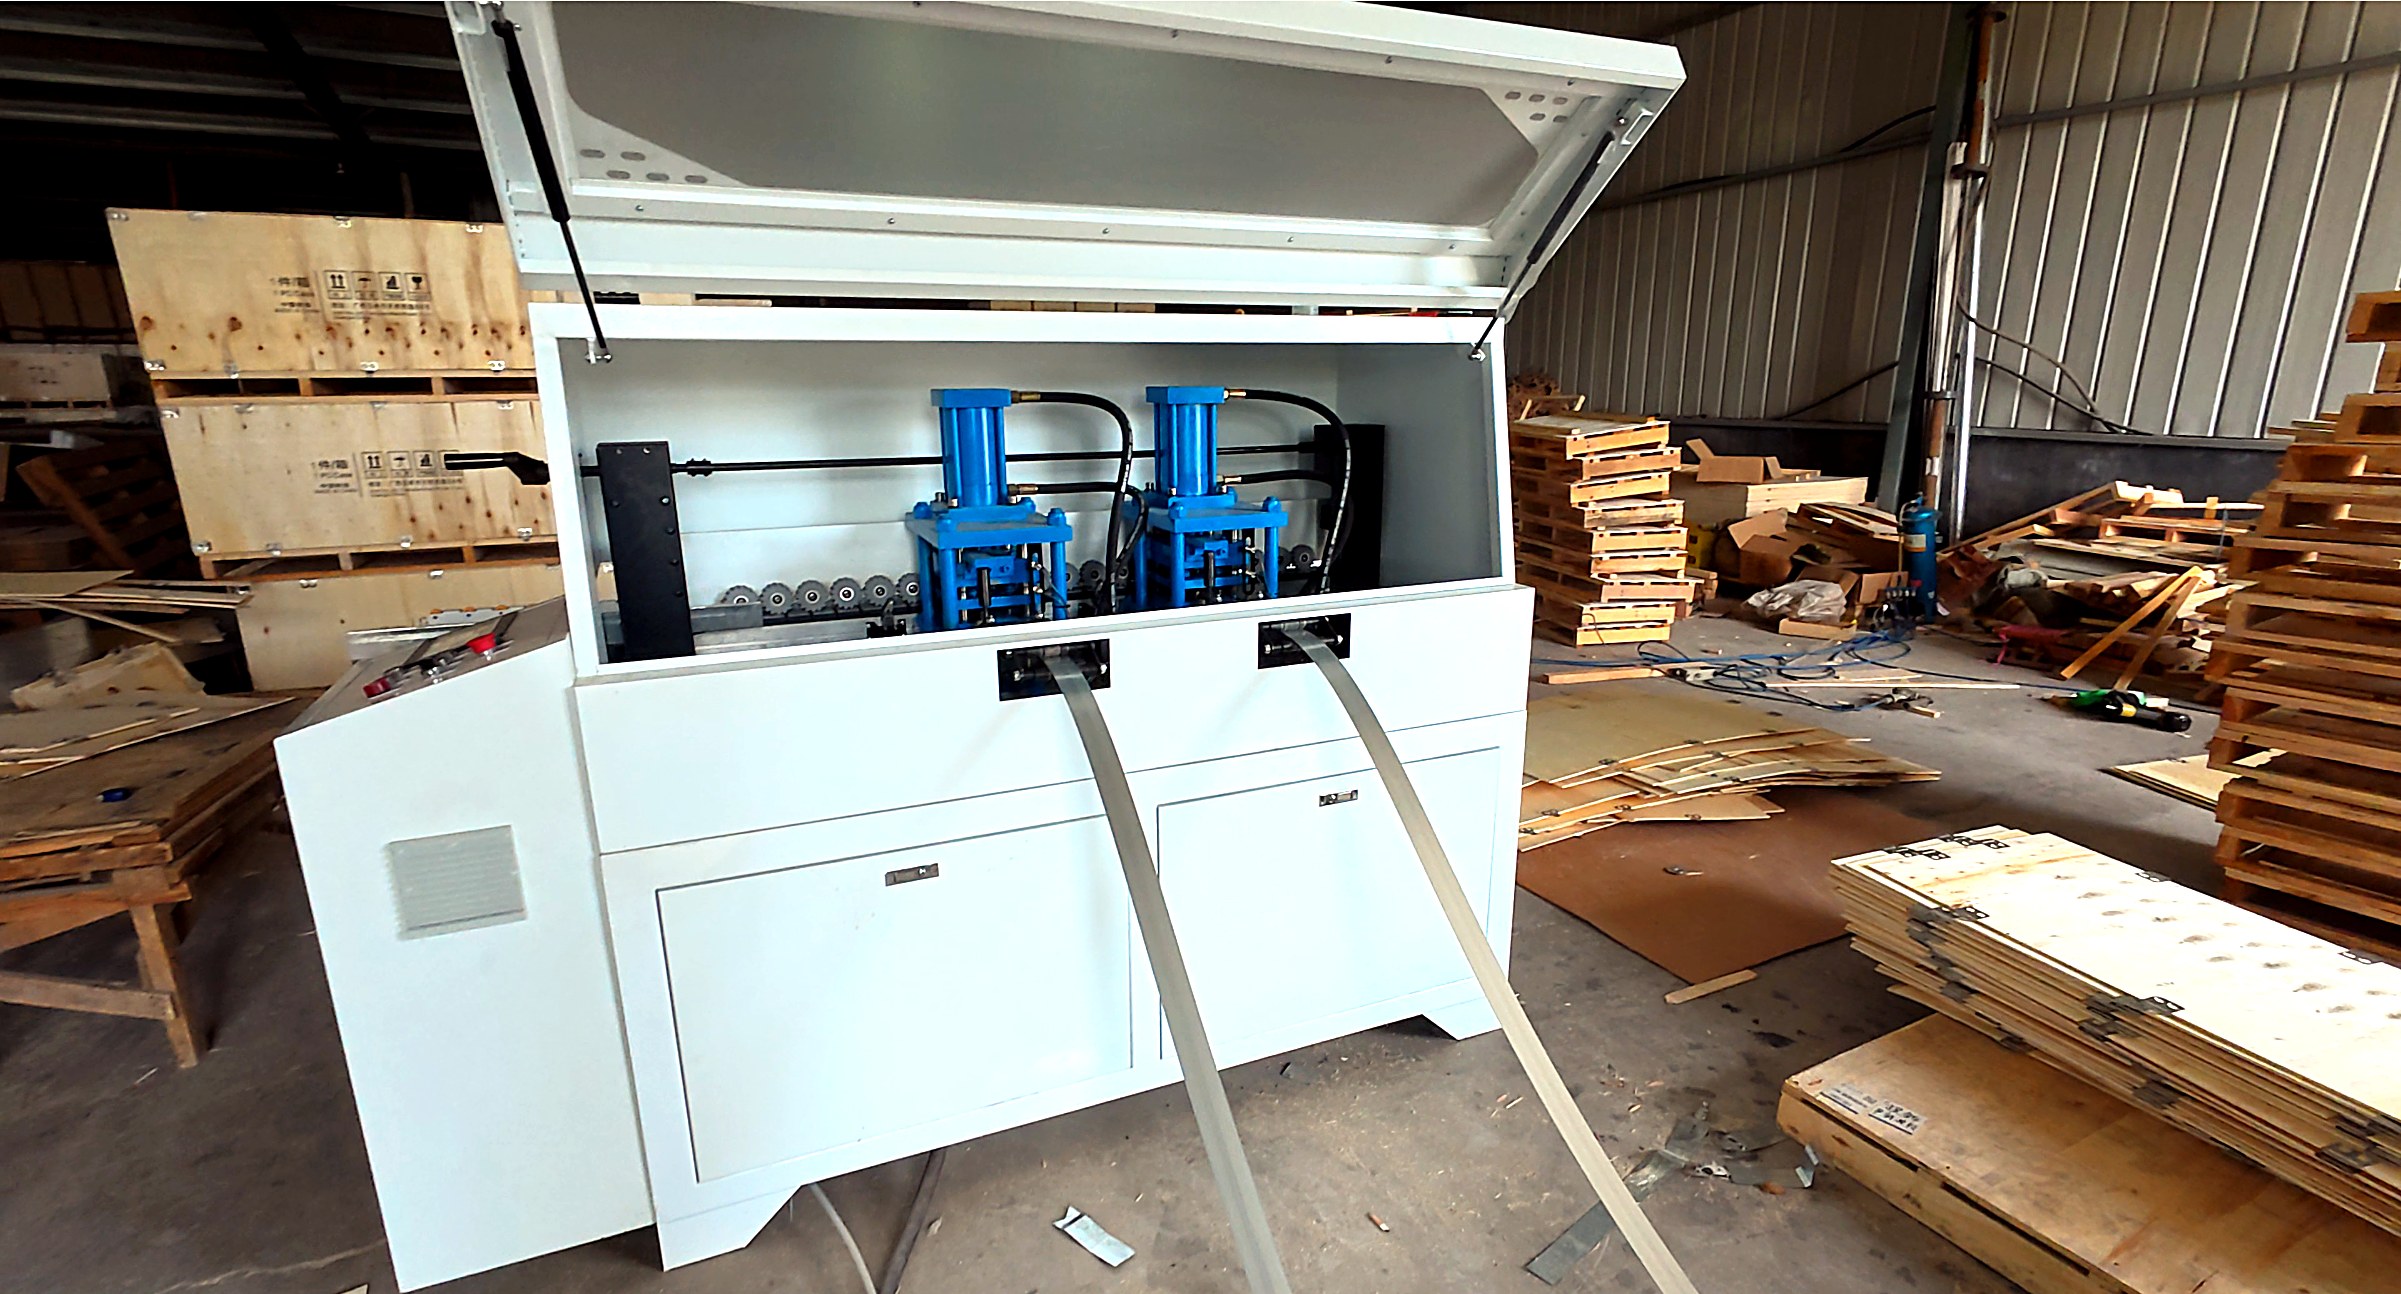
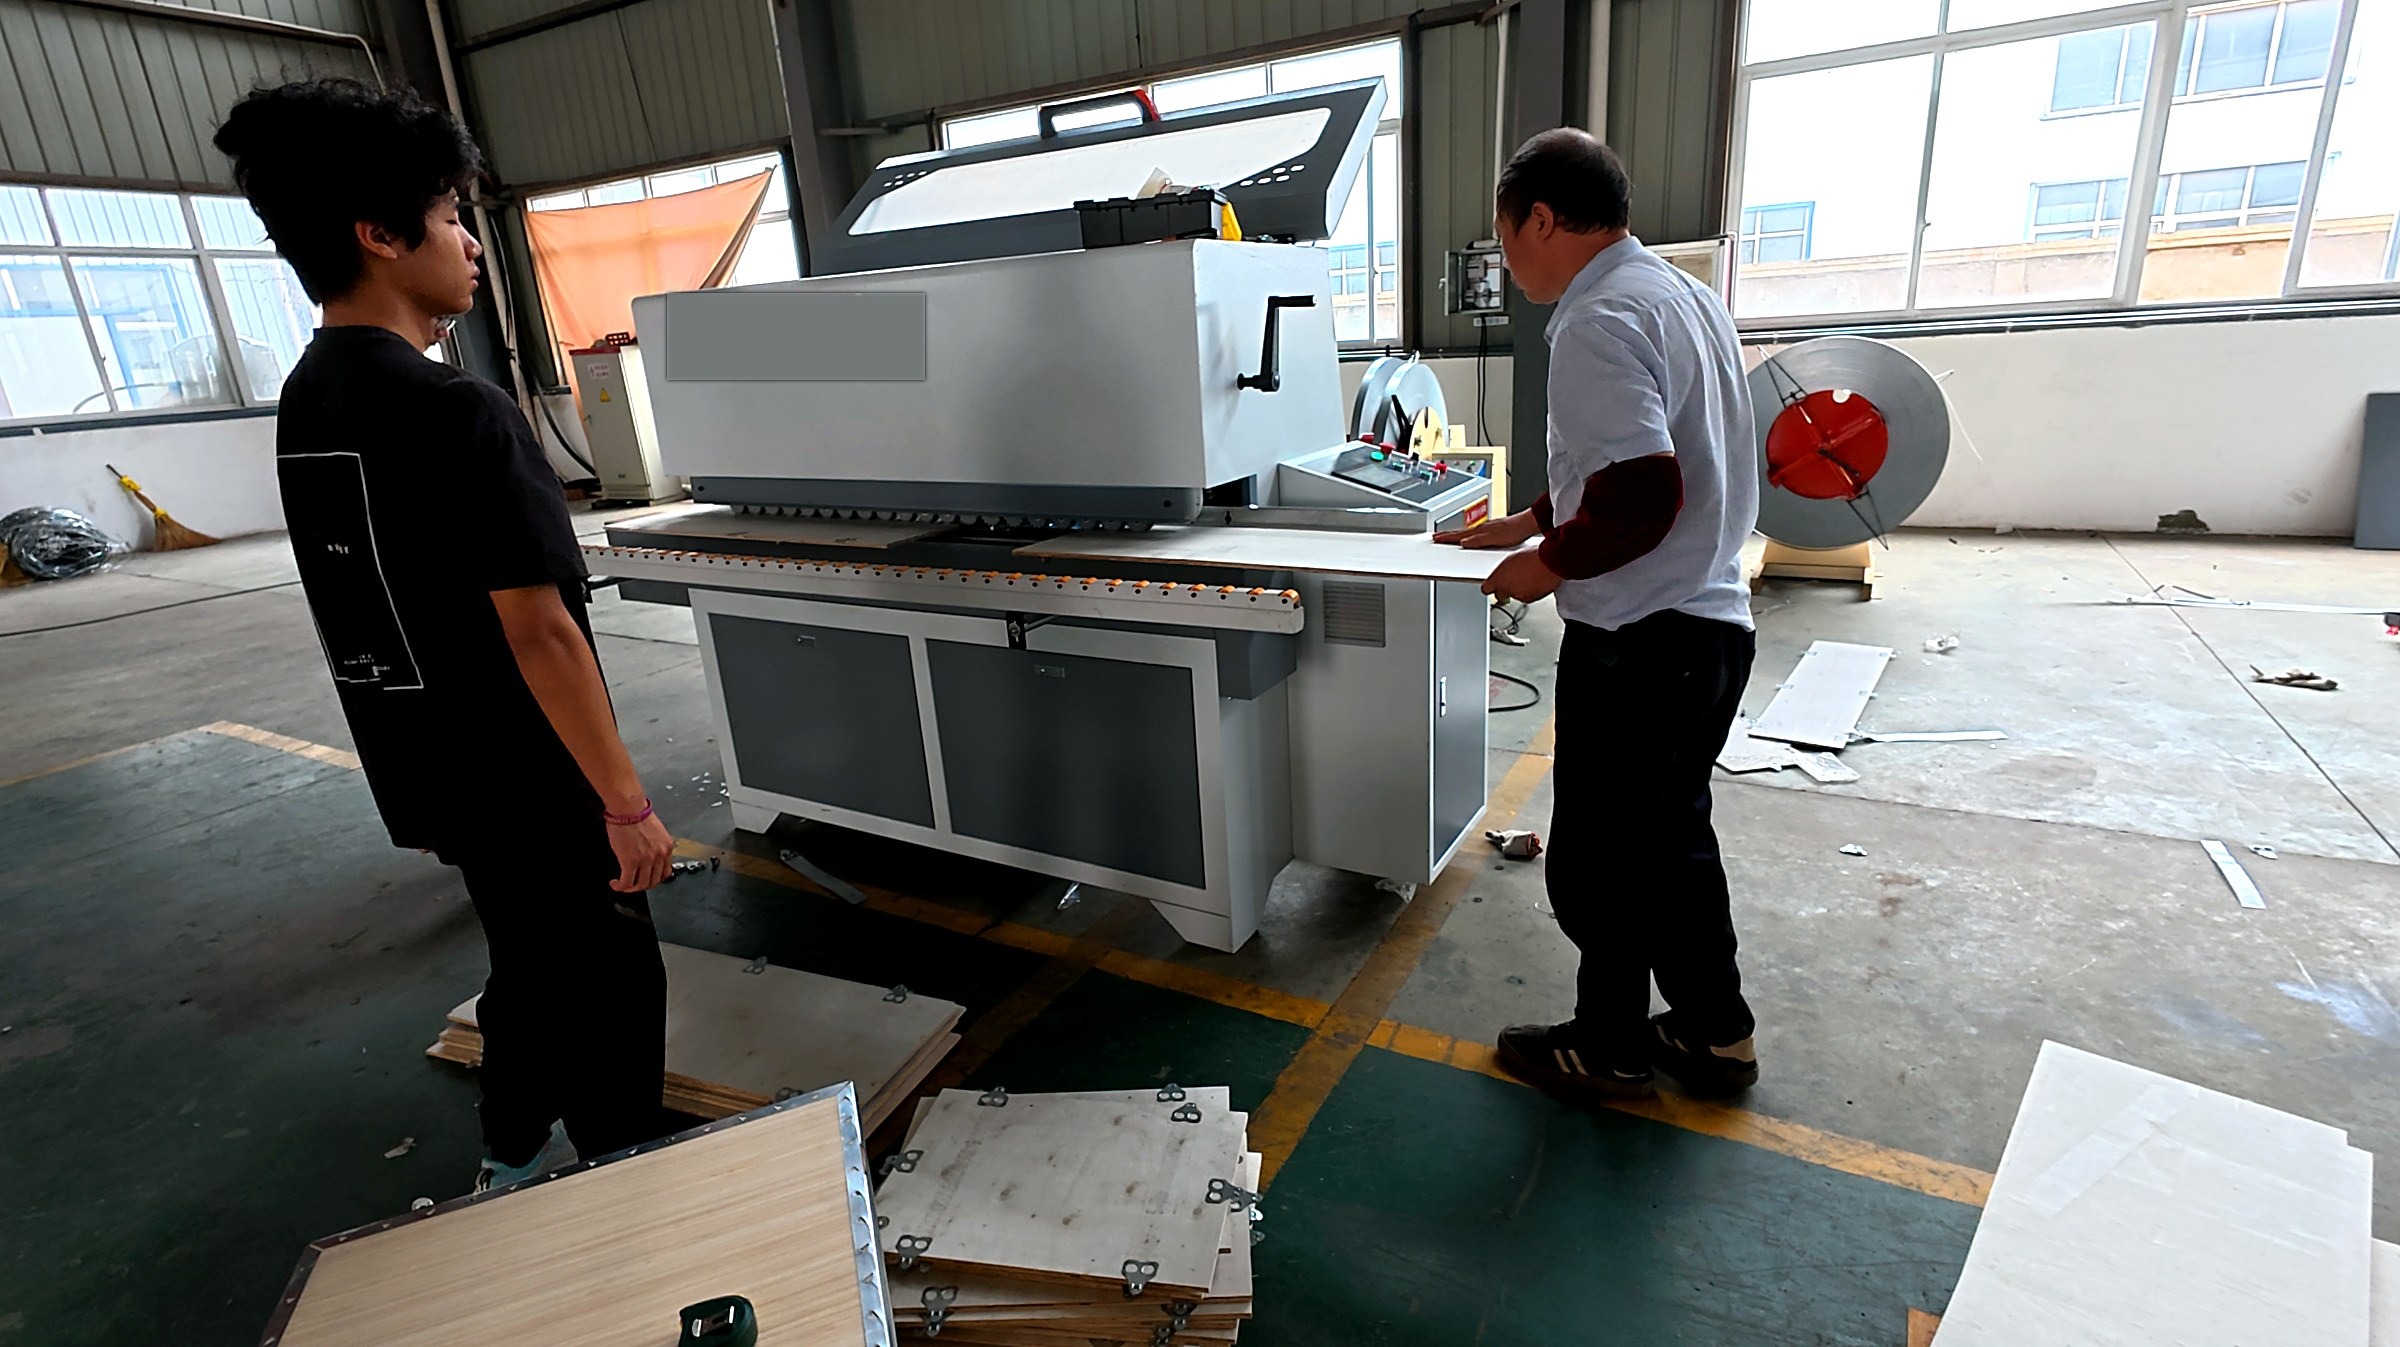
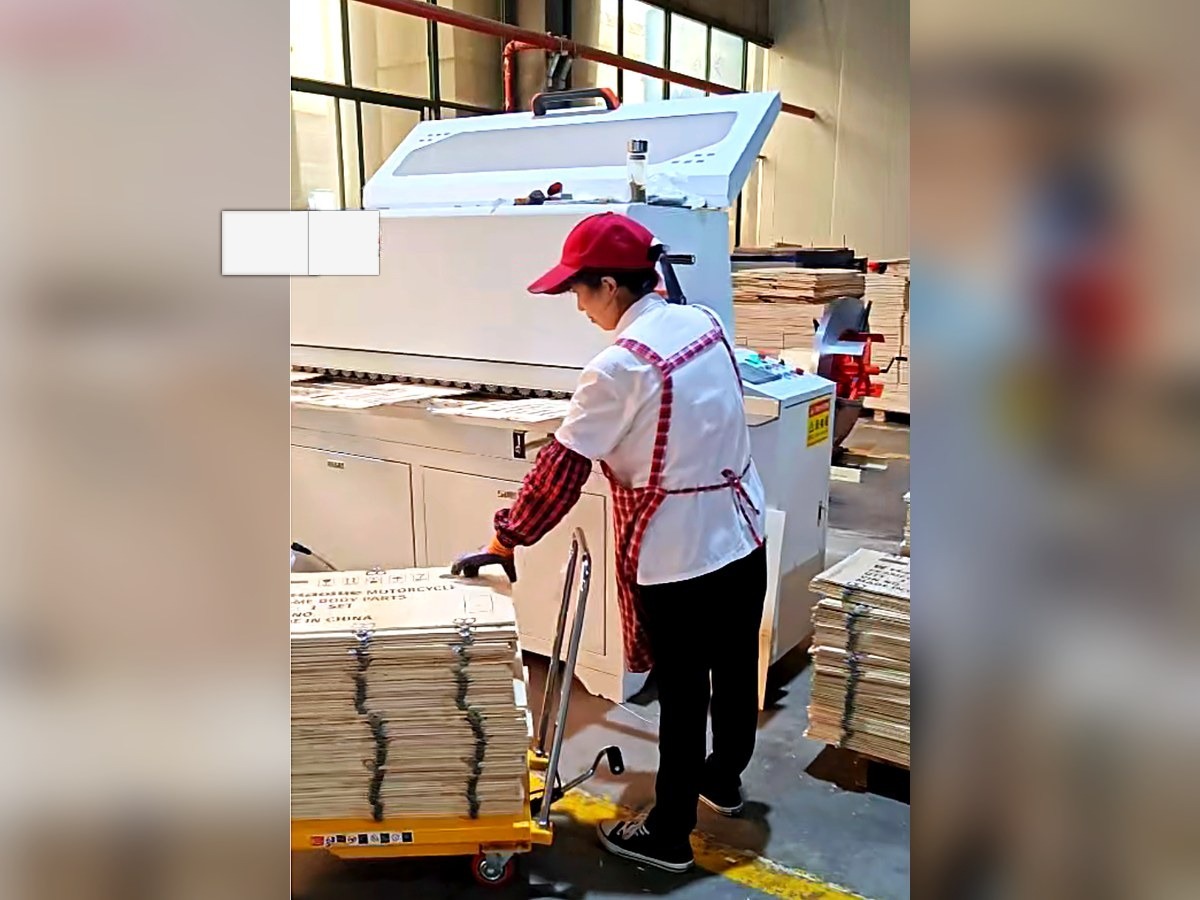
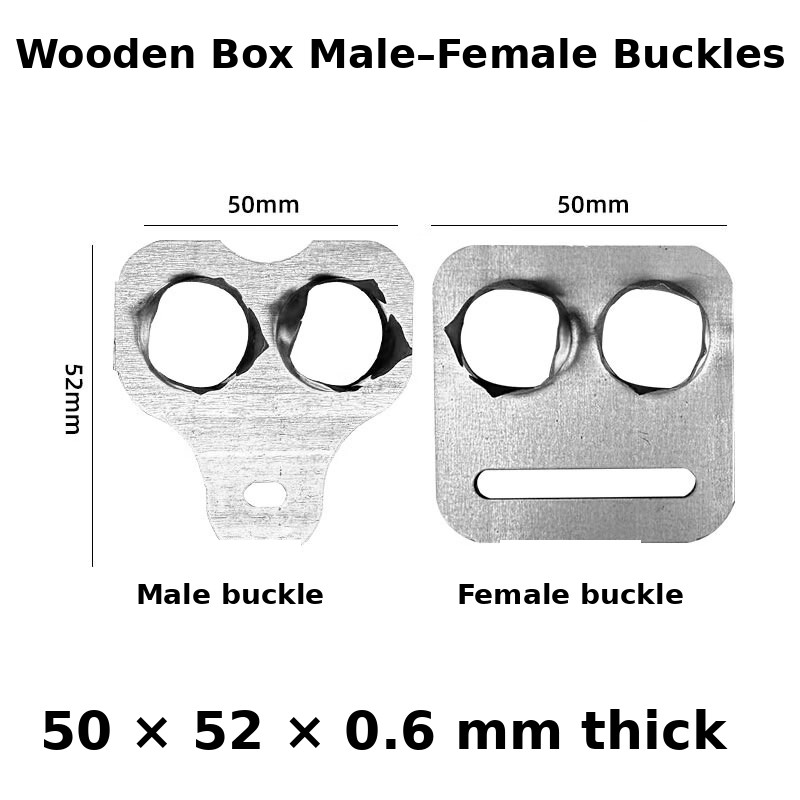
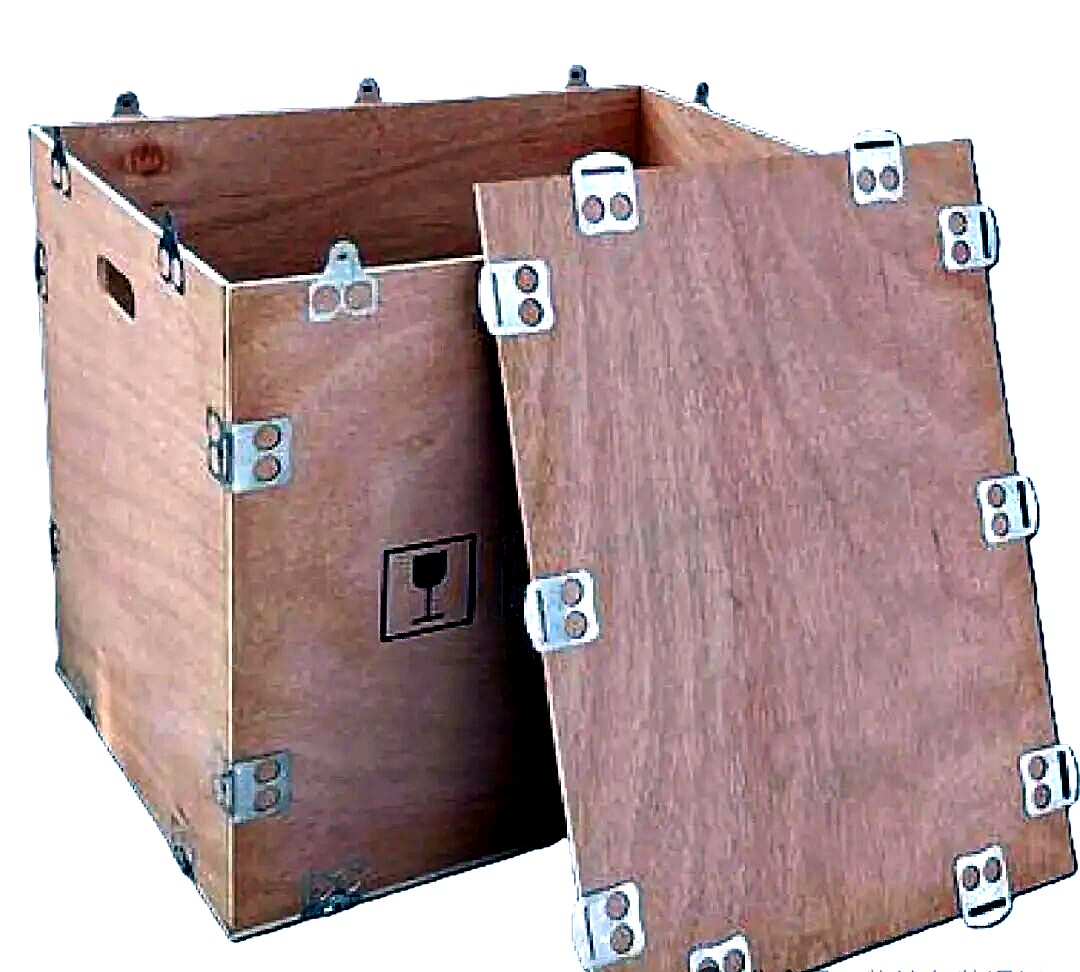
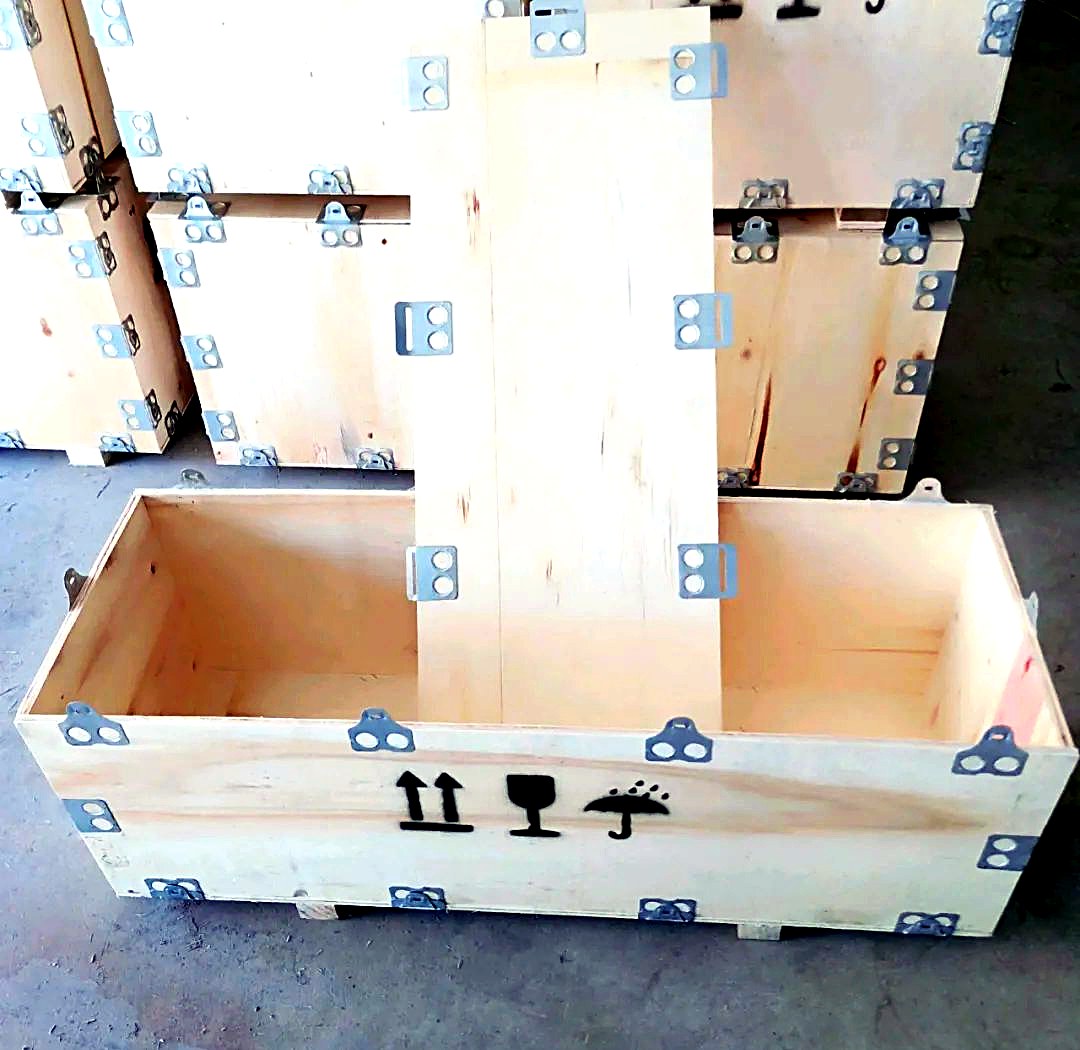
Standard configuration data. Machines are configured to order — contact us for values matched to your product.
| Model | DA-8000 series (male–female type) |
|---|---|
| Motor power | 6 kW |
| Fastening speed | 30–60 /min |
| Applicable steel strip width | 50 mm |
| Applicable panel thickness | 5–12 mm |
| Max. assembly length | 9,000 mm |
| Machine size (L×W×H) | 2,450 × 800 × 1,600 mm |
| Machine weight | 1,000 kg |
| Recommended working area | 3 × 3 m |
| Output | Male buckles + female buckles |
The standard configuration of the DA-8000 series. Alternative brands and upgraded configurations are available on request.
| Control system | PLC control system | Siemens, Germany |
|---|---|---|
| Servo drive & motor | Servo system | Inovance |
| Planetary reducer | Precision planetary reducer | Zhongda Leader |
| Hydraulic die assembly | 120 kg, triple-enlarged outlet design | |
| Female-buckle die | Additional die set for female buckles | |
| Hydraulic cylinder | Additional cylinder for female-buckle forming | |
| Bearings & screws | 304 stainless steel | |
| Springs | Precision die springs | Daido, Japan |
| Electrical components | Low-voltage electrics set | CHINT |
| Proximity switches | Position sensing set | Xinling |
| Dust protection | Full dust-proof design with cover | |
| Included accessories | 2 × automatic steel strip decoilers + feed rack |
The feeder delivers galvanized steel strip to the set position.
The panel is clamped and lined up precisely with the die.
The two die stations form and fasten male and female buckles one after the other.
The punches return and the workpiece moves on to the next cycle.
Look over the guards, chains, dies and feed tracks, and fit the male and female dies for the buckle set in use. Run the machine empty for 1–2 minutes and check that it runs smoothly and quietly.
Set the matched steel strip into the dies the right way round. Keep both feed tracks clear — no stacking, no jammed buckles.
Lay the plywood panel flat on the worktable and line the fastening point up with the center of the die. Hold the panel firm so it cannot move.
Press start: the two die stations form and fasten the male buckle and the female buckle one after the other, then reset on their own.
Work the box through each fastening point at a steady pace. Check every clasp: buckles flat, tight and matched, with no cracks or dents in the panel.
Run the machine empty for 10–20 seconds to clear the tracks, then stop and switch off. Clean the table, tracks and dies, and log the run.
Safety: keep hands out of the pressing, feeding and transmission zones while the machine runs. Stop immediately on jamming, unusual noise or a mis-fastened buckle — never run a faulty machine.